Reaction Distillation Unit

  • Home
  • Reaction Distillation Unit

Reaction Distillation Unit

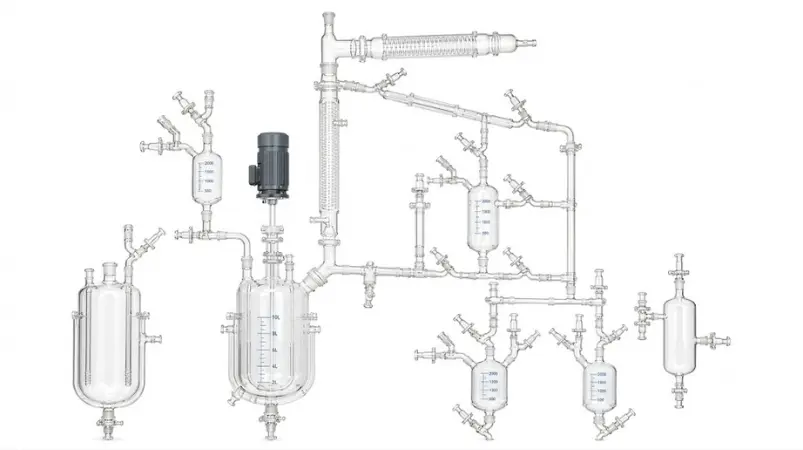
The Reaction Distillation Unit (RDU) is a high-efficiency integrated glass process system designed to perform chemical reaction and distillation simultaneously in a single unit. This advanced configuration combines the capabilities of a Reaction Unit, Fractional Distillation Unit, or a hybrid Reaction–Fractional Distillation System, making it ideal for pilot plants, R&D laboratories, and small-scale production facilities.

Manufactured using Borosilicate Glass 3.3, the unit ensures excellent chemical resistance, thermal stability, and contamination-free processing. It is suitable for operation under atmospheric pressure as well as full vacuum, offering maximum operational flexibility.

How Does the Reaction Distillation Unit Work? (Step-by-Step Process)

Charging of Reactants
Raw materials are charged into the spherical glass reactor through the addition vessel.

Controlled Heating / Cooling
A metal heating–cooling bath circulates thermal fluids to precisely control reaction temperature.

Simultaneous Reaction & Vaporization
As the chemical reaction proceeds, volatile components vaporize simultaneously.

Fractional Separation
Vapor pass through the packed column, enabling fractional separation based on boiling points.

Condensation
Separated vapor enter the coil-type condenser, converting vapors into liquid distillate.

Product Collection
Condensed product is collected in the receiver system, equipped with cooler, vent, drain, and vacuum valves.

Reflux Control
A reflux divider allows precise control over reflux ratio, improving separation efficiency.

Key Features & Benefits of Reaction Distillation Unit

  • Dual Functionality – Reaction + Distillation in one system
  • High Process Efficiency – Reduced solvent usage & processing time
  • Borosilicate Glass 3.3 Construction – Superior chemical & thermal resistance
  • Vacuum & Atmospheric Operation
  • Packed Column for Enhanced Separation
  • Mechanical Stirrer with Heavy-Duty Seal
  • Modular & Scalable Design
  • Ideal for Pilot Plant & R&D Applications

Safety & Operating Advantages

  • Explosion-safe glass construction
  • No metal contamination in product stream
  • Smooth internal surfaces reduce residue buildup
  • Leak-tested under vacuum conditions
  • Safe handling of corrosive & high-purity chemicals
  • Controlled reflux minimizes thermal runaway risks

Optional Accessories & Custom Add-Ons

  • Vacuum Pump & Vacuum Controller
  • Chiller / Cooling Circulator
  • Electronic or Mechanical Speed Variator
  • Additional Product Receivers
  • Solvent Recovery Integration
  • Digital Temperature & Pressure Monitoring
  • Customized Column Height & Packing

Technical Specifications – Reaction Distillation Unit

Standard Model Range (FRU Series)

Model

Reactor Capacity

Bath Power (kW)

Addition Vessel

Vapour Line

Condenser HTA (m²)

Cooler HTA (m²)

Receiver Size

FRU10

10 L

2.0

2 L

50 DN

0.10

0.10

2L / 5L

FRU20

20 L

4.0

2 L

80 DN

0.35

0.10

2L / 5L

FRU50

50 L

6.0

5 L

100 DN

0.50

0.20

5L / 10L

FRU100

100 L

9.0

10 L

150 DN

1.50

0.35

10L / 20L

FRU200

200 L

12.0

20 L

150 DN

1.50

0.35

10L / 20L

FRU300

300 L

18.0

20 L

225 DN

2.50

0.50

20L / 20L

FRU500

500 L

24.0

50 L

300 DN

4.00

0.70

50L / 50L

Applications of Reaction Distillation Unit

  • Pharmaceutical Intermediates
  • Fine & Specialty Chemicals
  • Agrochemical Processing
  • Solvent Recovery & Purification
  • Esterification & Transesterification Reactions
  • Pilot Plant Process Development

Industries We Serve

  • Pharmaceutical Manufacturing
  • Chemical & Petrochemical Industries
  • Research & Development Laboratories
  • API & Bulk Drug Plants
  • Academic & Government Research Institutes

Why Choose Our Reaction Distillation Unit?

  • Manufacturer & Exporter of Industrial Glass Process Equipment
  • Custom-Engineered Solutions
  • Proven Performance in Pilot Plants
  • After-Sales Technical Support
  • Worldwide Supply Capability

Frequently Asked Questions (FAQ)

Q1. What is the advantage of reaction distillation?
Reaction distillation improves conversion efficiency by continuously removing products as they form.

Q2. Can the unit operate under full vacuum?
Yes, the unit is designed for both atmospheric and full vacuum operation.

Q3. What material is used for construction?
All wetted parts are manufactured from Borosilicate Glass 3.3 with PTFE components.

Q4. Is customization possible?
Yes, vessel size, column height, condenser capacity, and accessories can be customized.


Related Products

Simple Distillation Unit

View Details

Reaction Distillation Unit

View Details

Fractional Distillation Unit

View Details

Continuous Distillation System

View Details