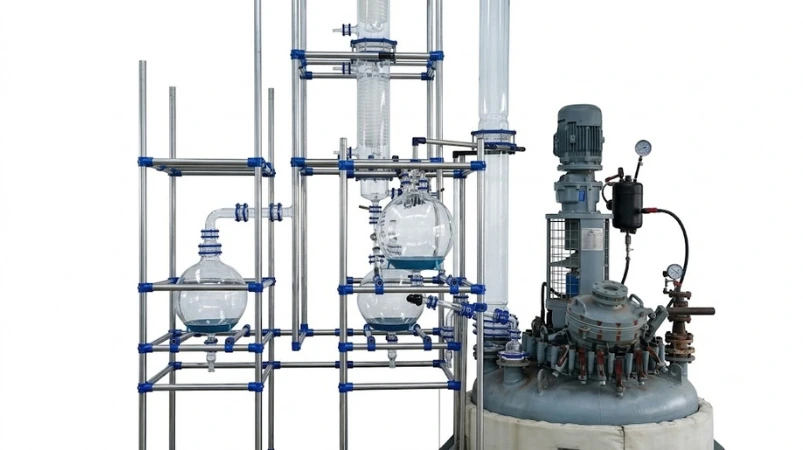
Distillation Overhead for Production

  • Home
  • Distillation Overhead for Production

Distillation Overhead for Production

The Distillation Overhead for Production is a high-performance industrial glass distillation system designed for continuous or semi-batch separation of chemical mixtures. It efficiently condenses and collects volatile fractions from large-scale distillation operations while maintaining precise temperature and pressure control. Constructed from borosilicate glass 3.3, this unit provides excellent chemical resistance, transparency, and operational safety, making it ideal for pilot plants, production units, and R&D setups.

Key Features & Benefits

  •  High-Efficiency Distillation: Optimized for collection of top fractions in large-scale operations
  •  Precise Process Control: Temperature and vapor management for reproducible distillation
  •  Borosilicate Glass Construction: Corrosion-resistant and transparent for process monitoring
  •  Modular & Scalable: Can be integrated into existing production lines
  •  Vapor Condensation & Reflux Control: Minimizes product loss and improves purity
  •  Compatible with Multiple Setups: Can be paired with reactors, extractors, or scrubbers

How Does It Work?

  • Vapor from the distillation vessel rises into the overhead condenser.
  • The vapor passes through a reflux divider and cooling section to condense selectively.
  • Condensed fractions are collected in receiver flasks or tanks.
  • Uncondensed gases may be recycled or vented through a gas scrubber.
  • The system can operate under atmospheric pressure or vacuum for sensitive products.

Technical Specifications

Parameter

Specification

Vessel Capacity

20 L – 500 L (depending on production needs)

Condenser Type

Coil, vertical or horizontal, glass-jacketed

Material

Borosilicate Glass 3.3, PTFE, SS Supports

Operating Temperature

Ambient – 200 °C (depending on product)

Pressure Range

Full vacuum to +1 bar(g)

Reflux Divider

Adjustable for precise fraction control

Receiver System

1–4 L glass receivers; optional collection tanks

Utilities Required

Cooling water, heating media, vacuum line

Optional Accessories

Reflux receiver, vacuum sensors, sampling ports, pH monitor, automation panel

Applications

Pilot plant distillation, chemical separation, essential oil recovery, solvent purification

Industries & Applications

  • Chemical & Fine Chemical Industry – Large-scale distillation, solvent recovery
  • Pharmaceutical Industry – Purification of active ingredients and intermediates
  • Essential Oil & Flavor Industry – Extraction and collection of volatile oils
  • Research & Pilot Plants – Process development and scale-up trials
  • Environmental Applications – Solvent recovery and emission control

Why Choose Our Distillation Overhead?

  •  High Purity Recovery with minimal product loss
  •  Transparent Design for real-time process monitoring
  •  Customizable & Modular to fit any production workflow
  •  Corrosion-Resistant Materials ensure long-term durability
  •  Optional Accessories for automation, sampling, and precise control

Optional Accessories & Customization

  • Adjustable reflux dividers for precise fraction separation
  • Glass or SS receivers for batch collection
  • Vacuum sensors and pressure gauges
  • Automation and control panels for process logging
  • Sampling ports and drain valves for operational convenience

Order Your Distillation Overhead Today!

In Stock – Limited Availability!
Bulk Discounts Available – Save More on Large Orders!
Customizable & Scalable – Ships Worldwide

Related Products

Distillation Overhead for Production

View Details

Gas Scrubber

View Details