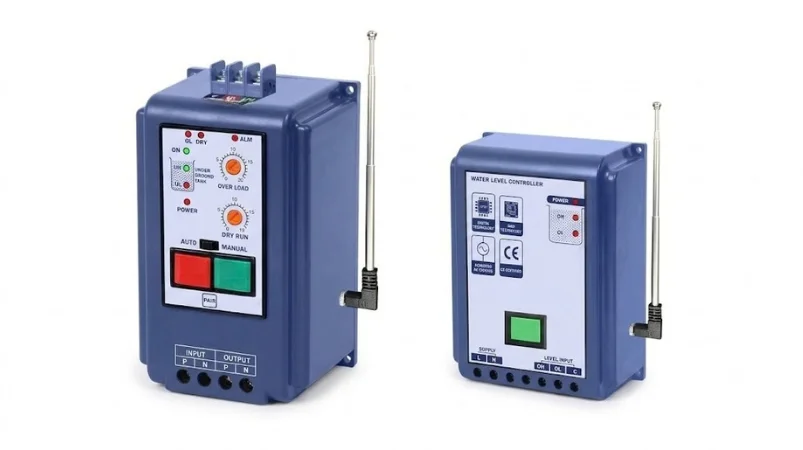
Automatic Level Controller

  • Home
  • Automatic Level Controller

Automatic Level Controller

The Automatic Level Controller is an industrial-grade electronic control device designed to automatically monitor, regulate, and maintain liquid levels in tanks, vessels, sumps, overhead tanks, underground tanks, reactors, and process systems.
It eliminates the need for manual supervision by automatically controlling pumps, motors, or solenoid valves, ensuring safe, efficient, and uninterrupted operation.

Widely used in industrial plants, chemical processing, pharmaceutical manufacturing, laboratories, water management systems, and process equipment, the Automatic Level Controller enhances operational safety, process efficiency, and equipment life.

How Does an Automatic Level Controller Work? (Step-by-Step Process)

  • Level Sensing
    Conductive probes or float sensors detect the liquid level inside the tank or vessel.
  • Signal Detection
    When the liquid reaches preset levels, the sensor sends a signal to the controller unit.
  • Logic Processing
    The controller processes the signal using predefined level logic.
  • Control Action
    The controller automatically switches ON or OFF the pump / valve to maintain the desired level.
  • Continuous Monitoring
    The system continuously monitors the liquid level in real time.
  • Safety Protection
    Prevents overflow, dry running, pump damage, and process interruption.

Key Features & Benefits – Automatic Level Controller

  • Fully automatic liquid level control
  • Prevents overflow and dry-run conditions
  • Compatible with conductive probes and float switches
  • Reliable relay-based output control
  • Compact panel-mount / wall-mount design
  • Low power consumption
  • Stable performance in industrial environments
  • Designed for continuous operation

Key Benefits

• Reduces manual monitoring
• Protects pumps and motors
• Improves system reliability
• Enhances process safety
• Minimizes water and liquid wastage

Technical Specifications – Automatic Level Controller

Parameter

Specification

Control Type

Automatic Level Control

Sensor Type

Conductive Probes / Float Switch

Number of Level Points

Single / Multi-Level (Configurable)

Output Type

Relay Output (Pump / Valve Control)

Power Supply

230V AC / 110V AC / 24V DC

Mounting

Panel Mount / Wall Mount

Operating Temperature

0°C to 55°C

Enclosure

Industrial ABS / Metal Housing

Protection

Electrical Noise & Surge Protection

Industries We Serve

  • Chemical & Petrochemical Plants
  • Pharmaceutical & API Manufacturing
  • Laboratories & Research Facilities
  • Water Treatment & Utility Systems
  • Glass Reactors & Process Equipment
  • Commercial & Industrial Infrastructure

Build Quality, Safety & Reliability

  • Industrial-grade enclosure for long life
  • Shock and vibration resistant design
  • Electrical surge and short-circuit protection
  • Safe isolation between sensing and control circuits

Designed for harsh industrial conditions and long-term reliable performance.

Installation, Wiring & Commissioning

  • Simple sensor wiring connections
  • Clearly marked terminal blocks
  • Easy pump / motor / valve connection
  • Quick installation and commissioning

No specialized tools or advanced technical skills required.

Applications – Automatic Level Controller

  • Overhead water tank control
  • Underground tank level management
  • Chemical storage tanks
  • Glass reactor liquid level control
  • Cooling water circulation systems
  • Process vessels, sumps, and reservoirs

Role in Level & Flow Control Systems

The Automatic Level Controller is a critical component of Level & Flow Control systems, ensuring consistent liquid availability, stable flow conditions, and automated process operation.

It supports process automation, equipment protection, and efficient liquid handling.

Energy Efficiency & Equipment Protection

  • Prevents pump dry running
  • Avoids unnecessary pump cycling
  • Reduces power consumption
  • Extends pump and motor life

This results in lower maintenance costs and improved operational efficiency.

Why Choose Our Automatic Level Controller?

  • Accurate and reliable level control
  • Industrial-grade build quality
  • Easy installation and maintenance
  • Energy-efficient operation
  • Custom configurations available
  • Bulk supply & OEM support

Trusted by industries, system integrators, and equipment manufacturers.

Frequently Asked Questions (FAQ)

Q1. What type of liquids can this controller handle?
It is suitable for water and conductive liquids. Sensor selection depends on the application.

Q2. Can it control both pumps and valves?
Yes, it can control pumps, motors, contactors, and solenoid valves.

Q3. Is it suitable for continuous operation?
Yes, it is designed for 24/7 continuous industrial operation.

Q4. Can the number of level points be customized?
Yes, single-level and multi-level configurations are available.

Q5. Does it protect against pump dry running and overflow?
Yes, it helps prevent both dry running and overflow conditions.

Operational Advantages

  • Improved process reliability
  • Reduced manual intervention
  • Lower operating and maintenance costs
  • Enhanced safety and automation

Related Products

Automatic Level Controller

View Details