Fractional Distillation Unit

  • Home
  • Fractional Distillation Unit

Fractional Distillation Unit

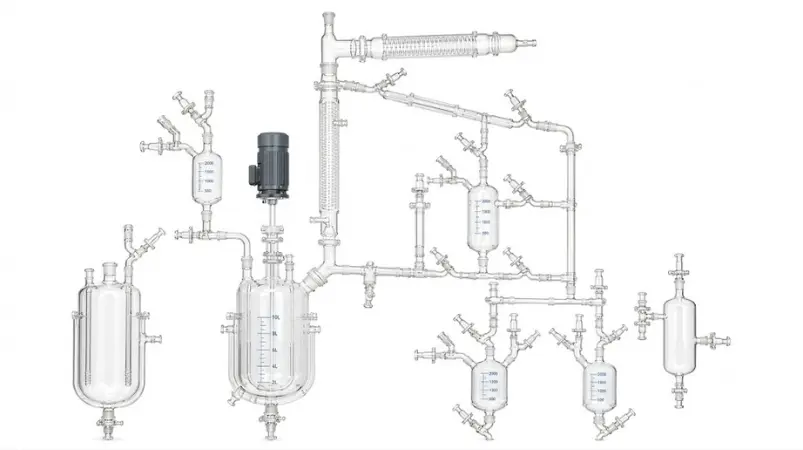
The Fractional Distillation Unit is a high-precision industrial glass distillation system designed for efficient separation of liquid mixtures with close boiling points. Built using Borosilicate Glass 3.3, this batch-type fractional distillation unit is widely used in chemical, pharmaceutical, petrochemical, and essential oil industries.

The system consists of a reboiler vessel mounted in a controlled heating bath, a packed fractional column, reflux divider, high-efficiency condensers, and product receivers. The reflux mechanism allows precise separation and higher product purity compared to simple distillation.

Our industrial fractional distillation unit is suitable for atmospheric as well as full vacuum operation and is available in 20 L to 500 L capacities, making it ideal for laboratory, pilot, and production-scale applications.

How Does a Fractional Distillation Unit Work? | Step-by-Step Process

  • Charging the Feed Material
    The liquid mixture is charged into the glass reboiler vessel, which is mounted inside a metal heating / cooling bath.
  • Controlled Heating
    The bath heats the mixture gradually, generating vapours of multiple components.
  • Fractional Separation in Packed Column
    Vapours rise through the packed fractional column, where repeated condensation and re-evaporation occur, improving separation efficiency.
  • Reflux Control
    Condensed vapours are partially refluxed back into the column using a reflux divider, enhancing purity.
  • Condensation & Sub-Cooling
    The top vapours pass through coil condensers and product coolers, ensuring complete condensation.
  • Product Collection
    • Top product is collected in receiver vessels
    • Bottom product is drained from the reboiler via a bottom drain valve
  • Vacuum Operation (Optional)
    Under vacuum, boiling points reduce, allowing safe processing of heat-sensitive materials.

Key Features & Benefits – Fractional Distillation Unit

Borosilicate Glass 3.3 Construction – High thermal & chemical resistance

Packed Fractional Column – Superior separation efficiency

Reflux Control System – Higher purity & yield

Atmospheric & Full Vacuum Operation

High-Efficiency Coil Condensers & Product Coolers

Modular & Scalable Design

Wide Capacity Range (20L–500L)

Suitable for Complex & Close Boiling Mixtures

Technical Specifications – Fractional Distillation Unit


Model

Capacity

Bath Power (kW)

Vapour Line

Condenser HTA (m²)

Cooler HTA (m²)

Receiver Size

FDU10

10 L

2.0

50 DN

0.2

0.1

2L , 2L

FDU20

20 L

4.0

80 DN

0.35

0.10

2L, 5L

FDU50

50 L

6.0

100 DN

0.50

0.20

5L, 10L

FDU100

100 L

9.0

150 DN

1.50

0.35

10L, 20L

FDU200

200 L

12.0

150 DN

1.50

0.35

20L, 20L

FDU300

300 L

18.0

225 DN

2.50

0.50

20L, 20L

FDU500

500 L

24.0

300 DN

4.00

0.70

50L, 50L

Operating Conditions:

  • Pressure: Atmospheric to Full Vacuum
  • Construction: Borosilicate Glass 3.3
  • Type: Batch-Type Fractional Distillation System

Safety & Operating Advantages – Fractional Distillation Unit

  • Explosion-Safe Glass Construction – Ideal for volatile solvents
  • Vacuum-Compatible Design – Low-temperature, safe distillation
  • No Metal Contamination – High-purity fractions
  • Uniform Heating & Controlled Reflux – Stable operation
  • Leak-Proof Joints & Precision Glass Fabrication
  • Easy Cleaning & GMP-Friendly Design

Optional Accessories & Add-Ons – Fractional Distillation Unit

  •  Vacuum Pump & Vacuum Controller
  •  Chiller / Cooling Circulator
  •  Digital Temperature & Pressure Controllers
  •  Additional Receiver Vessels
  •  Sampling Port & Sight Glass
  •  Integration with Solvent Recovery Systems

 Fully customizable based on process requirements

Industries We Serve

  • Pharmaceutical & API Manufacturing
  • Chemical & Fine Chemical Industry
  • Petrochemical Processing
  • Essential Oil & Aroma Chemical Industry
  • Perfume & Fragrance Manufacturing
  • Research Laboratories & Pilot Plants
  • Food & Beverage Processing

Applications of Fractional Distillation Unit

  • Separation of close-boiling components
  • High-purity solvent fractionation
  • Petroleum & hydrocarbon separation
  • Essential oil purification
  • Research & process development
  • Pilot-scale chemical production

Frequently Asked Questions (FAQ) – Fractional Distillation Unit

Q1. What is a Fractional Distillation Unit used for?

A Fractional Distillation Unit is used to separate complex liquid mixtures with similar boiling points using a packed column and reflux mechanism.

Q2. What is the difference between simple and fractional distillation?

Fractional distillation provides higher separation efficiency and purity compared to simple distillation, especially for close-boiling mixtures.

Q3. Can the unit operate under vacuum?

Yes, the unit supports both atmospheric pressure and full vacuum operation.

Q4. What capacities are available?

Available in 20 L, 50 L, 100 L, 200 L, 300 L & 500 L capacities.

Q5. Is customization possible?

Yes, capacity, column height, condenser area, reflux ratio, and automation can be customized.

Why Choose Our Fractional Distillation Unit?

  1. Manufacturer & Exporter of Industrial Glass Equipment
  2. Precision Flame-Worked Glass Fabrication
  3. Proven Industrial Performance
  4. Custom-Engineered Solutions
  5. Competitive Pricing & Global Supply

Related Products

Simple Distillation Unit

View Details

Fractional Distillation Unit

View Details

Continuous Distillation System

View Details

Reaction Distillation Unit

View Details