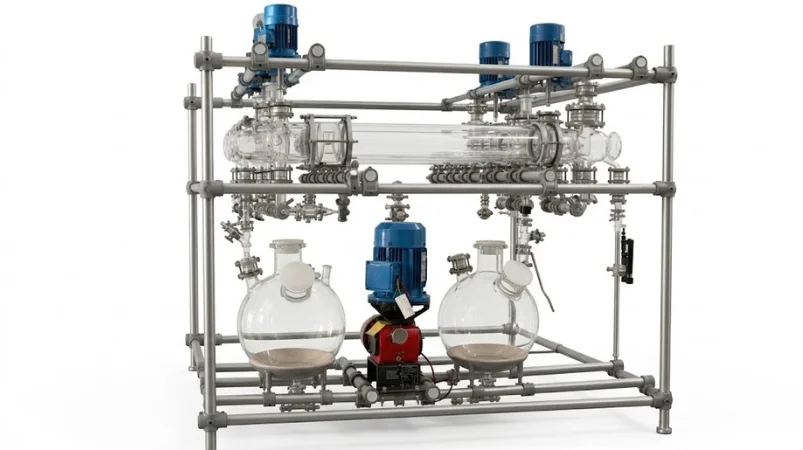
Mixer Settlers

  • Home
  • Mixer Settlers

Mixer Settlers

High-Efficiency Liquid-Liquid Separation Equipment

Mixer Settlers are a class of industrial process equipment designed for liquid-liquid extraction, widely used in hydrometallurgy and chemical processing industries. They provide precise separation of immiscible phases and are critical for industries such as copper, nickel, cobalt, uranium, and other metal extraction processes.

Working Principle of Mixer Settlers

A Mixer Settler combines mixing and settling in a controlled, sequential process:

  • Mixing Stage – Two immiscible liquids are combined in a horizontal or vertical mixing chamber. The dispersed phase interacts with the continuous phase to allow efficient mass transfer.
  • Settling Stage – After mixing, the mixture flows into a settling compartment where the liquids separate naturally by density difference.
  • Gravity Separation – The heavy and light phases are collected separately through gravity-driven outlets.

Continuous operation is achieved by connecting multiple mixer-settler stages in series or counter-current flow, improving extraction efficiency and throughput.

Key Features & Advantages

  • High Efficiency: Ensures maximum mass transfer and component separation.
  • Modular Design: Can be customized for single-stage or multi-stage extraction systems.
  • Versatile Applications: Suitable for extraction, washing, and stripping processes.
  • Low Maintenance: Minimal moving parts reduce wear and downtime.
  • Precise Phase Separation: Optimized coalescence rate for effective separation of dispersed phases.
  • Scalable: Applicable from laboratory to industrial-scale operations.

Applications of Mixer Settlers

  • Hydrometallurgy: Extraction of copper, nickel, cobalt, uranium, and other metals.
  • Chemical Processing: Liquid-liquid extraction of organic compounds.
  • Washing and Stripping Processes: Efficient removal of impurities or residual solvents.
  • Pharmaceuticals & Specialty Chemicals: Separation of active ingredients and reaction by-products.
  • Emulsion Formation: Controlled creation of permanent emulsions for chemical reactions.

Technical Highlights

  • Material of Construction: Borosilicate glass, PTFE, and corrosion-resistant alloys.
  • Flow Configuration: Horizontal or vertical stages with counter-current operation.
  • Design Considerations: Focus on dispersed phase coalescence, phase residence time, and efficient gravity separation.
  • Utility Requirements: Can operate with minimal utilities; optional heating/cooling for temperature-sensitive extractions.

Benefits of Using Mixer Settlers

  1. Maximizes recovery of valuable components from waste streams.
  2. Reduces chemical usage by efficient extraction.
  3. Enhances process sustainability through modular design and low utility consumption.
  4. Ensures consistent product quality even at large-scale production.
  5. Provides clear visual monitoring in glass variants, making troubleshooting easier.

Frequently Asked Questions (FAQs)

Q1: What is a Mixer Settler used for?
A: It is used for liquid-liquid extraction, washing, and stripping processes, especially in hydrometallurgy and chemical industries.

Q2: How many stages can be used in a Mixer Settler system?
A: The system can be single-stage or multi-stage, designed according to process requirements and feed concentration.

Q3: What materials are used for construction?
A: Borosilicate glass, PTFE, and corrosion-resistant metals are commonly used to ensure chemical compatibility.

Q4: Can Mixer Settlers handle large-scale industrial operations?
A: Yes, they are scalable from pilot labs to industrial-scale production while maintaining high efficiency.

Q5: Are Mixer Settlers easy to maintain?
A: Yes, they are designed with minimal moving parts for easy cleaning and low maintenance.

Mixer Settlers provide an efficient, reliable, and customizable solution for industrial-scale extraction and liquid-liquid separation. Their modular design, scalability, and chemical compatibility make them a preferred choice for hydrometallurgical and chemical industries.

Related Products

Glass Absorber Systems

View Details

Mixer Settlers

View Details